Technical Knowledge
Curing Time Management of Dry-Applied Materials Under Different Climatic Conditions
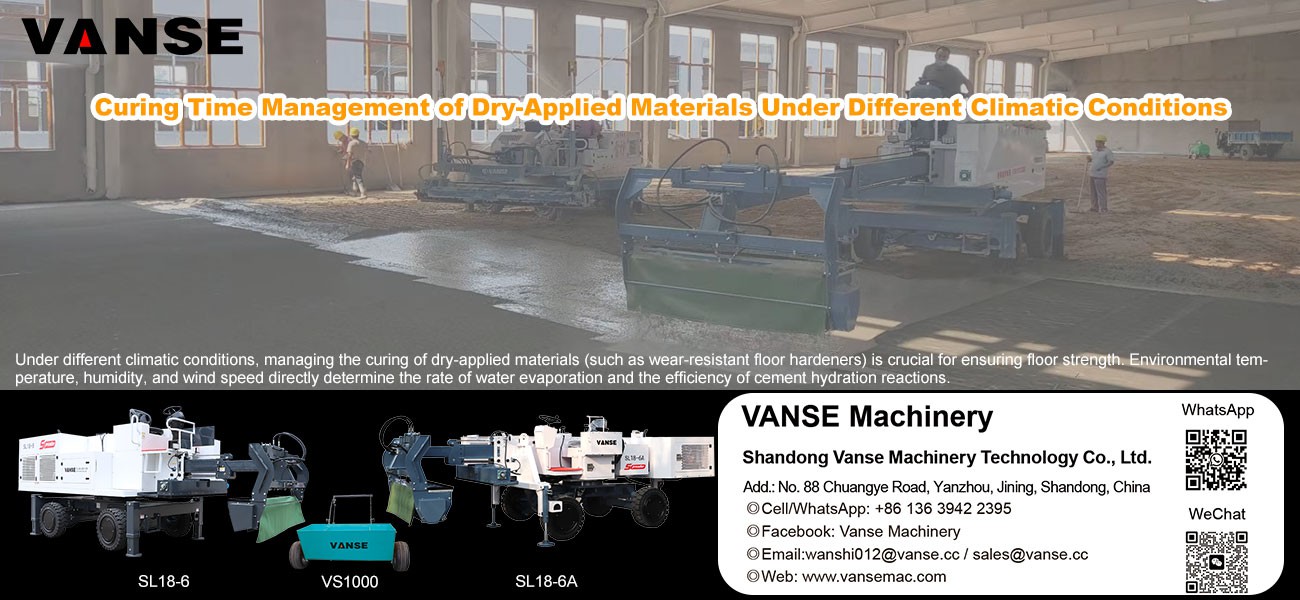
Under different climatic conditions, managing the curing of dry-applied materials (such as wear-resistant floor hardeners) is crucial for ensuring floor strength. Environmental temperature, humidity, and wind speed directly determine the rate of water evaporation and the efficiency of cement hydration reactions.
The following are curing time management strategies for different climatic conditions:
1. High Temperature and Dry Climate (>30°C, Low Humidity)
In this environment, water loss is extremely rapid, easily leading to cracking or delamination of the dry-applied material.
Curing time management: Shorten the "water absorption waiting period" after dry application. Begin troweling immediately after the material darkens (indicating absorption of moisture from the base layer) to prevent the material from failing to bond with the base layer due to rapid water loss.
Core operation: Increase spraying or use film curing to ensure stable dissipation of hydration heat.
2. Low Temperature and Cold Climate (<5°C)
Low temperatures significantly slow down the hydration reaction of cement, leading to a substantial increase in curing time.
Curing Time Management: Extend the monitoring period for initial and final setting times. When the temperature approaches 0°C, heating or insulation measures must be taken; otherwise, the dry-mix material may freeze and fail before complete curing.
Key Operation: Strictly control the amount of dry-mix material to prevent premature cessation of bleeding from the base layer, which would prevent the material from being properly wetted.
3. High Humidity/Rainy Climate (Humidity > 80%)
In high-humidity environments, water evaporation is extremely slow, and the surface tends to remain wet or even accumulate water for extended periods.
Curing Time Management: Appropriately extend the time before using the power trowel to prevent premature finishing, which can lead to bubbles or peeling on the surface.
Core Operation: Enhance ventilation to aid in water evaporation. If working outdoors, strictly monitor rainfall forecasts, as uncured material will be washed away by rain.
Reference table showing the influence of environmental parameters on the curing process.
| Climate Types | Water evaporation rate | Curing speed | Key Management Points |
| Hot and dry | Very high | Very fast | Prevent cracking, expedite construction, and ensure proper wet curing. |
| Cold winters | Very low | Slow | Strengthen insulation and prevent frost damage. |
| Humid and rainy | Low | Slower | Control the timing of finishing work and enhance ventilation. |
Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.
Thanks to All the Friends Who Support and Trust Shandong Vanse Machinery Technology Co., Ltd.
If you want to know more about Shandong Vanse Machinery Technology Co., Ltd. or have any questions, please feel free to contact us:
Our Factory
Shandong Vanse Machinery Technology Co., Ltd.
Share this article
About the Author: Shandong Vanse Machinery Technology Co., Ltd.
Shandong Vanse Machinery Technology Co., Ltd. is a high-tech manufacturer specializing in concrete construction machinery, including laser screeds and related equipment. The company integrates R&D, production, and global sales, with products exported to over 60 countries and widely used in infrastructure projects worldwide.
Previous Post
Next Post
Related Articles
You Might Also Like
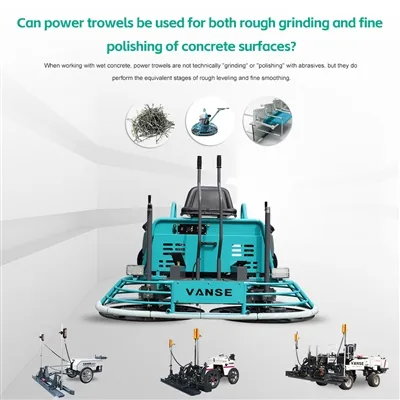
Can power trowels be used for both rough grinding and fine polishing of concrete surfaces?
When working with wet concrete, power trowels are not technically "grinding" or "polishing" with abrasives, but they do perform the equivalent stages of rough leveling and fine smoothing. Rough Stage (Floating): During the initial passes, operators attach large metal float pans (or flat float blades) to the bottom of the trowel. This step knocks down high spots, pushes coarse aggregates below the surface, and brings the concrete paste (cream) to the top. Fine Stage (Finishing): Once the concrete has stiffened, the pans are removed to expose the finish blades. The operator pitches these blades at an angle. The friction from the spinning, angled blades burnishes the surface, closing the pores to create a dense, smooth, and hard finish. In recent years, the industry has developed specialized tooling that allows standard power trowels (especially heavy ride-on models) to be retrofitted for true abrasive grinding and polishing on fully cured concrete slabs. Rough Grinding: You can equip the trowel's rotors with specialized rotary attachments that hold low-grit metal-bonded diamond abrasives (e.g., 30 to 50 grit). This setup is highly effective for removing surface impurities, smoothing out micro-roughness, and preparing the floor for liquid densifiers. Fine Polishing: By progressively swapping out the tooling for higher-grit resin diamond pads (ranging from 400 up to 3000 grit), the power trowel can rapidly polish the cured concrete to a high-gloss, glass-like finish. While using a power trowel for polishing cured concrete is incredibly fast and cost-effective for massive warehouse floors, it does have a distinct limitation compared to traditional planetary floor grinders. Light Downward Pressure: Power trowels distribute their weight over a very wide area. They are excellent for polishing the top "cream" layer of the concrete but lack the concentrated, heavy head pressure required to grind deep into the slab to expose large aggregates. Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.Repair And Maintenance Methods Of Concrete Laser Leveling Machine (1)
As an important equipment for modern floor construction, the stability and service life of concrete laser leveling machine are crucial to construction efficiency and quality. In order to ensure the normal operation of the concrete laser leveling and extend its service life, regular repair and maintenance are essential. This article will introduce in detail the repair and maintenance methods of the concrete laser leveling, including daily equipment inspection, laser system calibration, blade and scraper maintenance, hydraulic system maintenance, electrical system inspection, filter and oil replacement, machine body cleaning and protection and storage and transportation precautions. ☆♦☆ Daily inspection of equipment ☆♦☆ Daily inspection of equipment is the basic work for the repair and maintenance of concrete laser leveling. Its purpose is to discover and deal with potential problems in time to ensure the normal operation of the equipment. Daily inspections mainly include the following: 1. Check the appearance of the equipment to ensure there is no obvious damage, deformation or corrosion. 2. Check whether the connecting bolts of each component of the equipment are tight and not loose. 3. Check the hydraulic oil tank, fuel tank and lubricating oil level to ensure that the oil level is within the normal range. 4. Check the wear of wearing parts such as blades and scrapers. If there is any wear, replace it in time: 5. Check the working status of key components such as the laser system and electrical system to ensure their normal operation. ☆♦☆ Laser system calibration ☆♦☆ The laser system is the core component of the concrete laser leveling machine, and its accuracy is directly related to the flatness of the floor. Therefore, regular calibration of the laser system is very necessary. The main steps for laser system calibration are as follows: 1. Use professional laser calibration instruments to calibrate the laser transmitter and receiver to ensure accurate propagation of the laser beam. 2. Check whether the laser reflector is clean and unobstructed to ensure it is working properly. 3. Adjust the height and angle of the laser leveler according to the actual situation to ensure that the laser beam is parallel to the ground. ☆♦☆ Blade and scraper maintenance ☆♦☆ Blades and scrapers are important wearing parts of concrete laser levelings, and their performance directly affects the construction quality of the floor. In order to extend the service life of blades and scrapers and improve construction efficiency, they need to be maintained regularly. Maintenance measures mainly include: 1. Check the wear of the blade and scraper. If there is any wear, replace it in time. 2. Clean the blades and scrapers regularly to remove concrete residue and dirt on the surface. 3. Apply an appropriate amount of grease on the surface of the blade and scraper to reduce friction and wear. ☆♦☆ Hydraulic system maintenance ☆♦☆ The hydraulic system is the power transmission system of the concrete laser leveling. Its stability and reliability are crucial to the normal operation of the equipment. The main contents of hydraulic system maintenance include: 1. Regularly check the oil level and quality of the hydraulic oil tank, and promptly replenish or replace the hydraulic oil if necessary. 2. Clean the filter and radiator of the hydraulic system to prevent clogging and overheating. 3. Check whether the connections of the hydraulic pipelines are tight and there is no leakage. 4. Regularly inspect and maintain hydraulic pumps, motors and valves to ensure their normal operation. ☆♦☆ Electrical system inspection ☆♦☆ The electrical system is the control system of the concrete laser leveling, and its stability and safety are crucial to the normal operation of the equipment. The main contents of electrical system inspection include: 1. Check whether the connection between cables and connectors is tight and free of damage or looseness. 2. Check the working status of electrical components such as sensors, switches and relays to ensure their normal operation, 3. Dust and clean the electrical system regularly to prevent dust and moisture from affecting electrical components. ☆♦☆ Filter and oil replacement ☆♦☆ The cleanliness and performance of the filter and oil directly affect the operating efficiency and service life of the concrete laser leveling. Therefore, regular replacement of filters and oil is very necessary. Please pay attention to the following points when replacing: 1. Select the appropriate filter and oil model according to the requirements of the equipment manual. 2. When replacing the filter, make sure that the new filter is of the same model as the old filter and is installed correctly. 3. When replacing oil, ensure the cleanliness of the fuel tank and oil circuit to prevent impurities and moisture from entering the fuel tank. 4. When replacing filters and oil, pay attention to safe operations to avoid oil splashing and fire accidents. ☆♦☆ Body cleaning and protection ☆♦☆ Body cleaning and protection are important measures to keep the appearance of the concrete laser leveling machine clean and extend its service life. Main tasks include: 1. Regularly clean the soil and dirt on the outer surface of the equipment to keep the equipment clean. 2. Carry out anti-rust treatment on the surface of the equipment to prevent rust and corrosion. 3. Perform periodic inspections and repairs on the paint and coating of the equipment to maintain its beauty and durability. 4. When parking the equipment, choose a dry and ventilated place to avoid the impact of moisture and high temperature on the equipment. ☆♦☆ Storage and transportation precautions ☆♦☆ Storage and transportation are inevitable links in the use of concrete laser leveling machines. Correct storage and transportation methods are of great significance to protect the equipment from damage and increase its service life. The following points need to be noted when storing and transporting: 1. When storing the equipment, ensure that the equipment is in a horizontal state to avoid tilting or collapse. 2. For equipment stored for a long time, it should be started and operated regularly to keep the moving parts of the equipment in good condition. 3. When transporting equipment, use professional transportation tools and fixtures to ensure the stability and safety of the equipment during transportation. 4. Avoid transporting equipment under harsh road conditions and climate conditions to reduce the impact and vibration of the equipment during transportation. To sum up, the repair and maintenance of concrete laser leveling machines involves many aspects, and factors such as the equipment's use environment, workload, and maintenance cycle need to be comprehensively considered. By implementing the above repair and maintenance methods, you can ensure the normal operation of the concrete laser leveling and extend its service life, thereby improving construction efficiency and quality. At the same time, these measures will also help reduce equipment failure rates and maintenance costs, creating greater economic benefits for enterprises.Cement Floor Cracks: Cause Analysis and Prevention
Cracks in cement floors (typically referring to cement concrete surfaces, such as indoor floors, outdoor plazas, and parking lots) not only affect appearance but can also reduce durability and even hinder functionality due to water seepage and debris accumulation. The following detailed analysis covers common crack symptoms, core causes, and targeted prevention and control measures to help accurately identify and effectively resolve the problem. The form, width, and distribution of cement floor cracks directly reflect their causes and can be categorized as follows: Crack Types Appearance Characteristics Common Locations Hazard Level Surface Cracks Cracks are short and thin (<0.1mm wide), forming an irregular network with no discernible depth, mostly concentrated in the surface layer (1-3mm deep). Large indoor floors and outdoor plazas Low (appearance only, no structural risk) Vertical/Horizontal Cracks Cracks are long (several to tens of meters long), straight, 0.1-0.5mm wide, and can penetrate the surface layer (5-10mm deep). Along the length/width of the floor, or along both sides of a partition joint Medium (easy to seep, accelerating surface degradation) Cracks at the Edges and Corners of Plates Cracks extend from the corners of the slab (such as the corners of a square floor) toward the center, forming an L-shaped or diagonal pattern, with a width of 0.2-0.8mm. At the joints of indoor and outdoor floor panels, near wall corners High (likely to cause edge peeling, affecting pedestrian safety) Through-Breaking Cracks Cracks extend through the entire cement surface layer (even penetrating the base layer), are >0.5mm wide, and are sometimes accompanied by slight ground subsidence or sanding. Highly loaded areas (such as parking lots and warehouses), and areas with uneven subgrades Extremely High (may cause floor damage and water accumulation, requiring urgent attention) The root cause of cement floor cracking is "internal stress in the surface layer exceeding its tensile strength." The sources of this stress are related to five key factors: material, base layer, construction, environment, and usage. The details are as follows: Improper material selection or proportioning directly leads to insufficient crack resistance in the surface layer: Incorrect cement selection: Using cement with a high heat of hydration (such as P.O. 42.5R rapid-hardening cement) to cast large surfaces releases a large amount of heat during hydration, raising the internal temperature of the surface layer. Contraction upon cooling creates "temperature stress," which can cause longitudinal and transverse cracks. Using expired cement (which has reduced strength) can also lead to insufficient tensile strength in the surface layer, making it more susceptible to cracking. Poor aggregate grading: If the fine aggregate (sand) is too fine (fineness modulus <2.3) or the mud content is too high (>3%), the cement requirement will increase (more cement paste is needed to coat the aggregate), leading to increased shrinkage of the surface layer. If the coarse aggregate (stone) is too small (<5mm) or missing, it will not form a "skeletal support," resulting in unrestrained shrinkage of the surface layer and prone to network cracking. If the water-cement ratio is too high: In pursuit of fluidity during construction, water usage is often blindly increased (water-cement ratio > 0.55). After the surface layer hardens, excess water evaporates, creating internal voids and reducing density. This significantly increases shrinkage (approximately 20% increase in shrinkage for every 0.1 increase in water-cement ratio), which can easily lead to surface cracking and edge cracking. Improper admixtures/admixtures: Failure to add or incorrect addition of admixtures (e.g., failure to add a retarder in summer, resulting in rapid initial setting of the surface layer and inability to grout after surface water evaporates; failure to add an antifreeze in winter, resulting in internal structural damage after freezing); and failure to add admixtures such as fly ash and mineral powder (key to reducing hydration heat and shrinkage) result in poor crack resistance in the surface layer. Cement floor surfaces rely on the stable support of a base layer (such as a lime soil base, crushed stone base, or concrete base). Base layer problems can directly affect the surface layer: Uneven base layer settlement: If the base layer is not compacted layer by layer during construction (e.g., a lime soil base with a compaction level less than 95%), or if there is a weak soil layer beneath the base layer (e.g., uncompacted backfill), the surface layer can experience partial subsidence during use, subjecting it to tensile stress and causing through-hole cracks or cracks at the edges and corners of the slabs. Uneven/contaminated base layer surface: The base layer surface has a height difference greater than 5mm (not leveled). The surface layer has uneven thickness after pouring, with thinner areas shrinking faster than thicker areas, creating "temperature differential stress." Oil and loose dust on the base layer surface have not been cleaned, resulting in insufficient adhesion between the surface layer and the base layer. After hardening, the two separate, and the surface layer shrinks independently, causing cracks. No isolation layer is provided for the base layer: When the base layer is concrete or a rigid material, without an insulating layer such as polyethylene film, the surface layer adheres too tightly to the base layer. During shrinkage, it is constrained by the base layer and cannot deform freely, causing cracks in areas of stress concentration (such as corners and joints). Construction operation is critical to crack control. Common mistakes include: Improper pouring and vibration: Failure to follow the "staged pouring, gradual progress" principle during pouring (e.g., large areas of ground are not divided into blocks, with individual blocks >20 m2), resulting in no channels for the surface layer to shrink as a whole; insufficient vibration during vibration (low density in some areas of the surface layer, insufficient tensile strength) or over-vibration (aggregate sinks, cement slurry floats, forming a "floating slurry layer" on the surface. After hardening, the floating slurry shrinks and cracks, known as crazing). Incorrect timing of surface calendering: Calendering too early (the surface layer has not yet set and the cement slurry has not yet developed strength) can easily cause sanding on the surface; calendering too late (the surface layer has already set and a crust has formed on the surface) can damage the surface structure, forming microcracks that later expand into cracks. Inadequate or improper sizing of the slurry: Large areas of flooring (single floor area >15 m2) are not provided with standardized expansion joints (spacing: ≤6 m vertically, ≤8 m horizontally). This lack of "stress relief" during surface shrinkage can lead to vertical/transverse cracks along weak areas (such as the center). Insufficient expansion joint depth (<1/3 of the surface layer thickness) or inadequate filler (such as asphalt mortar) can cause cracks to extend along both sides of the expansion joints. Untimely/inadequate curing: Failure to cover and cure the surface layer within 12 hours of pouring (e.g., exposure to direct sunlight in summer or wind in winter) allows surface moisture to evaporate rapidly, preventing internal moisture from being replenished. This results in "shrinkage stress" and causes surface cracking. Insufficient curing time (<7 days) prevents the surface layer from reaching its designed strength (typically ≥70% strength), leading to premature loading (e.g., pedestrians or vehicles), which can easily lead to corner cracks or through-hole cracks. Ambient temperature and humidity fluctuations can exacerbate stress in the surface layer and induce cracks: Severe Temperature Fluctuations: In summer, during daytime pouring (ambient temperature 35°C), the temperature drops sharply at night (15°C). The surface layer cools and contracts rapidly, while the interior cools and contracts slowly. This internal constraint creates "temperature stress" on the surface, leading to longitudinal, straight cracks. In winter, if the surface layer freezes before reaching its frost resistance (≥70% of design strength), the internal moisture freezes and expands, and upon thawing, the volume contracts, forming "freeze-thaw cracks" (mostly cracks at the edges and corners of the slabs, accompanied by surface spalling). Chronic and unstable humidity: In humid environments (such as bathrooms and underground garages), the surface layer absorbs moisture over time, softening the cement paste and reducing its tensile strength. In dry environments (such as heated rooms and warehouses in northern China), moisture from the surface layer continuously evaporates, accumulating shrinkage stress. The alternating effects of these two factors can easily lead to surface cracking or through-hole cracks. Improper load or maintenance during use can accelerate the development of cracks: Premature loading or overloading: Heavy objects (such as furniture and building materials) are piled on the surface before it reaches its design strength (28 days), or vehicles are driven on it (for example, a parking lot is opened to traffic without proper maintenance). This causes the surface to be subjected to loads exceeding its tensile strength, leading to through-cracks or cracks along the edges of the slabs. Lack of routine maintenance: Failure to promptly seal small cracks in the surface allows rainwater and oil to seep in, eroding the surface's internal structure. Furthermore, in winter, the water that seeps in freezes and expands, causing cracks to widen. Prolonged exposure to heavy loads (such as frequent forklift traffic in a warehouse) can lead to localized stress concentrations, causing longitudinal cracks. The core of prevention and control lies in "source control (materials + base layer), process control (construction), and post-maintenance (environment + use)." It is divided into two parts: "preventive measures" and "crack repair measures": Precise Material Selection: Prioritize cement with low hydration heat (such as P.O. 42.5 ordinary cement or slag Portland cement); use well-graded medium sand (fineness modulus 2.3-3.0, mud content ≤3%) and 5-10mm continuously graded crushed stone (mud content ≤1%) as aggregates; add Grade I fly ash (15%-20%) or mineral powder (20%-25%) to reduce hydration heat and shrinkage. Strictly control the water-cement ratio: The water-cement ratio should be ≤ 0.5 (for standard floors) and ≤ 0.45 (for impermeable floors). If necessary, add a retarding water reducer (at a dosage of 0.5%-1%) to maintain fluidity while reducing water consumption and minimizing shrinkage risk. Ensure the base layer is compacted and leveled: The base layer (lime soil/gravel) should be constructed in layers, with each layer ≤30cm thick and a compaction level ≥95% (tested using the knife ring method). The base layer surface should be leveled with cement mortar, with a height difference ≤3mm and cleaned (free of oil stains and loose dust). Apply a primer if necessary (to enhance adhesion between the surface layer and the base layer). Installing Isolation Layers and Expansion Joints: For rigid base layers (such as concrete), lay a 0.1mm thick polyethylene film isolation layer. For base layers >10m long, install expansion joints every 6-8m along the length (20mm wide and filled with asphalt hemp) to prevent base layer shrinkage from transferring to the surface layer. Scientific pouring and vibrating: For large floor areas, pour in blocks, with each block ≤15 m2 (rectangular blocks, aspect ratio ≤1.5). Leave 20 mm wide joints between blocks (the joint depth should be 1/3-1/2 the surface layer thickness). Vibrate with a flat vibrator (at a speed of 1-1.5 m/min) until the surface is free of bubbles and slurry. Avoid missed or over-vibration. Choose the right timing for calendering: Calender in three steps: ① Before initial setting (after the surface layer has absorbed water), smooth it with a wooden trowel; ② After initial setting (no visible finger marks remain), perform initial compaction with an iron trowel; ③ Before final setting (when the surface is nearly hardened), perform final compaction with an iron trowel to ensure a smooth surface without any marks. Strengthened maintenance management: Cover the surface with geotextile or plastic film (add a shade net in summer and a thermal blanket in winter) within 12 hours after pouring to keep the surface moist. Curing time for ordinary surfaces is ≥7 days, and for impermeable/load-bearing surfaces is ≥14 days. Pedestrians and vehicles are prohibited from entering during the curing period. Temperature Control: In summer, avoid pouring at noon (select morning and evening temperatures between 25-30°C). Cover the surface to maintain moisture. In winter, preheat the aggregate (≥5°C) before pouring, ensure the surface is at least 10°C before pouring, and maintain an ambient temperature of ≥5°C during curing (use heating if necessary). Usage and Management: The surface should be cured for 28 days before use. Premature stacking of heavy objects is prohibited. In areas such as parking lots and warehouses, limit vehicle/cargo weight to the designed load capacity to avoid local overloading. Regularly inspect the floor surface and seal any minor cracks with epoxy resin glue. If cracks have already appeared, first clean them (remove debris and dust, and flush with a high-pressure water gun), then repair them as follows: Crack Types: Repair methods Material Selection Key Points: Surface cracks Surface sealing method Epoxy sealer, cement-based penetrating crystallization coating (CCCW) Use a brush to evenly apply the glue/paint to the crack surface and a 5cm area on either side. Repeat 2-3 times. Cure for 24 hours. Vertical/horizontal cracks (width < 0.5mm) Low-pressure grouting method Cement slurry (water-cement ratio 0.45), epoxy slurry Drill an 8mm diameter hole (5mm deep) every 20cm along the crack. Insert a grouting tube and inject grout using a low-pressure pump (0.2-0.3MPa) until the grout overflows. Cure for 7 days. Cracks along edges and corners (width 0.2-0.8mm) Painting mortar filling method Polymer cement mortar (cement: sand: latex = 1:2:0.15) Chisel away the loose surface layer on both sides of the crack (5-10cm wide, 3-5mm deep). Clean and apply a primer. Fill with mortar and compact. Cure for 7 days. Through cracks (width > 0.5mm) Grouting + reinforcement method High-strength epoxy slurry, carbon fiber cloth First, fill the crack with high-pressure grouting (1.0-1.5MPa). Then, apply carbon fiber cloth (15cm wide, along the crack). Apply a topcoat. Cure for 14 days. The key to preventing and controlling cracks in cement floors is "prevention is better than cure": By optimizing the material mix (controlling the water-cement ratio and adding admixtures), stabilizing the base layer (compacting, leveling, and insulating layers), and standardizing construction (block-by-block pouring, timely maintenance, and appropriate gridding), stress can be reduced at the source. If cracks have already occurred, appropriate repair methods should be selected based on the crack morphology (width, depth, and location) to prevent further crack expansion. Paying attention to load control and regular maintenance during daily use can significantly extend the service life of cement floors. Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.