Technical Knowledge
Economic Value Analysis of Superflat Floors in VNA (Very Narrow Aisle) Warehouses
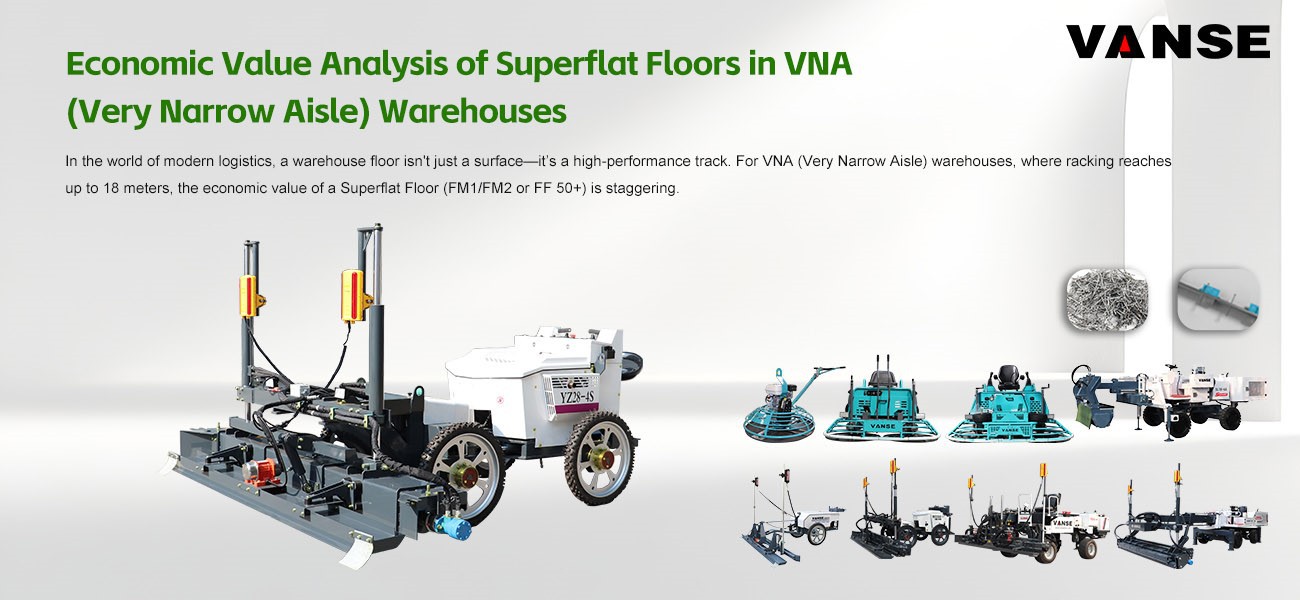
In the world of modern logistics, a warehouse floor isn't just a surface-it’s a high-performance track. For VNA (Very Narrow Aisle) warehouses, where racking reaches up to 18 meters, the economic value of a Superflat Floor (FM1/FM2 or FF 50+) is staggering.
A 1mm deviation at the base of a VNA forklift can translate into a dangerous 15cm "sway" at the top of the mast. If you’re a facility owner or developer, here is why investing in the "Vanse standard" for flooring isn't an expense-it’s a massive ROI driver.
1. Increased Throughput (Efficiency = Revenue)
In a VNA warehouse, the speed of the forklift is limited by the flatness of the floor. On a standard floor, trucks must slow down to avoid vibration and mast-lean.
The Economic Lift: A Superflat floor allows trucks to operate at maximum speed. This can increase "picks per hour" by 20% to 40%. In a high-volume logistics hub, that speed translates into millions of dollars in additional annual revenue.
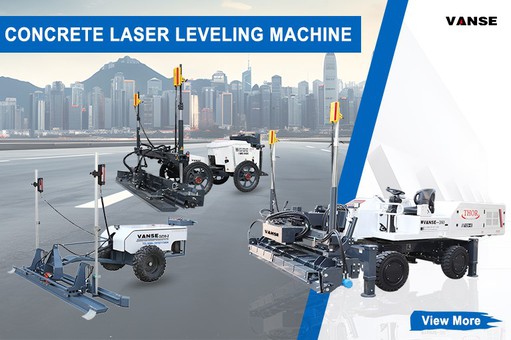
The Vanse Edge: To hit these numbers, the floor must be leveled with surgical precision. The Vanse YZ30-4E Telescopic Boomed Laser leveling allows for the long-strip pours essential for VNA lanes, ensuring the "track" is perfect from end to end without the "tire tracks" that traditional machines leave behind.
2. Massive Maintenance Savings (OpEx Reduction)
VNA trucks are expensive pieces of machinery with sensitive electronic components and high-pressure tires.
The Economic Lift: Bumpy floors cause "shock loading" on forklift axles and wear out tires 3x faster. A Superflat floor can reduce annual maintenance costs for a fleet of VNA trucks by up to 50%.
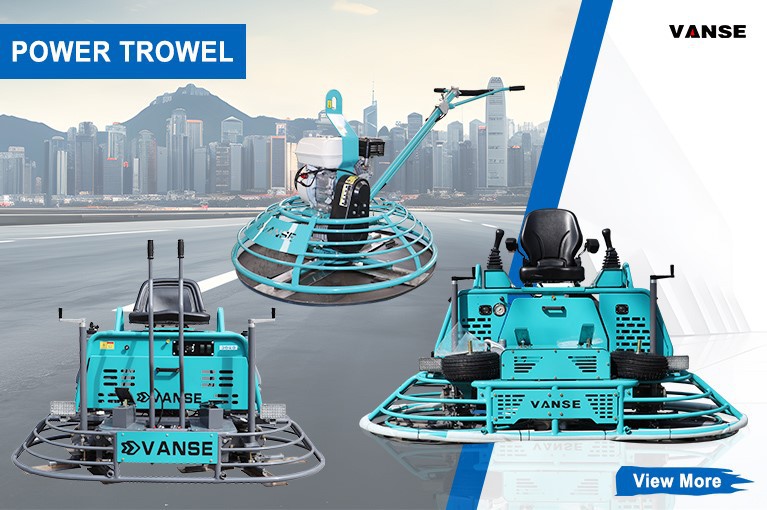
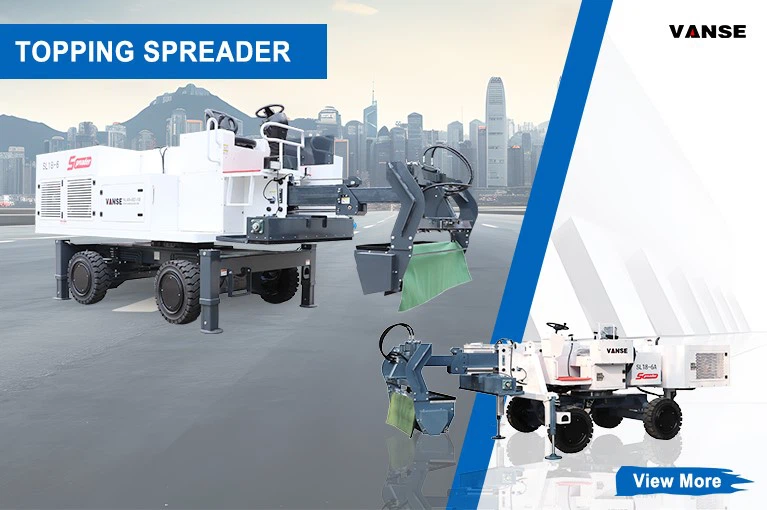
The Vanse Edge: Surface durability is just as important as flatness. By using a Vanse Automatic Topping Spreader to apply wear-resistant hardeners uniformly, followed by the high-torque burnishing of a Vanse VS1046H Ride-on Power Trowel, you create a rock-hard finish that won't "spall" or "dust," protecting your trucks for decades.
3. Maximum Space Utilization (Real Estate ROI)
The whole point of VNA is to pack more pallets into a smaller footprint.
The Economic Lift: Without a Superflat floor, you simply cannot use VNA racking safely. A high-quality floor enables you to build higher and narrower, potentially increasing your pallet capacity by 30% within the same building footprint.
The Vanse Edge: For multi-story or tight-access warehouses, the Vanse Mini Dumper and Concrete Distributor allow for precise material placement without disturbing the subgrade, ensuring that even the most difficult-to-reach bays meet the Superflat spec.
Economic Comparison: Standard vs. Vanse-Leveled Superflat Floor
| Feature | Standard Industrial Floor | Vanse Superflat (FM1/VNA) |
| Forklift Speed | Limited (40-60% capacity) | Maximum (100% capacity) |
| Truck Maintenance | High (Vibration damage) | Low (Smooth operation) |
| Space Density | Wide Aisles / Lower Racks | VNA Aisles / High-Bay Racks |
| Project Risk | High (Potential for grinding) | Low (Hit the spec first time) |
| Joint Integrity | Often spalled/ragged | Clean with Floor Saws |
The "Vanse Solution" for High-Value Flooring
When you browse www.vansemac.com, you’re not just looking at machines; you’re looking at Profitability Tools.
YZ Series Laser leveling: Hit the FF/FL specs that VNA trucks require.
Topping Spreaders: Guarantee the wear-resistance needed for repetitive wheel paths.
Power Trowels: Provide the dense, burnished finish that resists high-pressure tire wear.
Concrete Cutting Machines: Protect your joints from the heavy point-loads of VNA traffic.
Final Word
In the logistics world, the floor is the "engine room" of the business. A cheap floor is a constant drain on your profits through slow speeds and high maintenance. A Vanse-leveled Superflat floor is a one-time investment that pays dividends every single hour your warehouse is in operation.
Don't let your floor be a bottleneck. Visit Vanse Machinery today to see how we can help you maximize the economic value of your warehouse.
Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.
Thanks to All the Friends Who Support and Trust Shandong Vanse Machinery Technology Co., Ltd.
If you want to know more about Shandong Vanse Machinery Technology Co., Ltd. or have any questions, please feel free to contact us:
Our Factory
Shandong Vanse Machinery Technology Co., Ltd.
Share this article

About the Author: Shandong Vanse Machinery Technology Co., Ltd.
Shandong Vanse Machinery Technology Co., Ltd. is a high-tech manufacturer specializing in concrete construction machinery, including laser screeds and related equipment. The company integrates R&D, production, and global sales, with products exported to over 60 countries and widely used in infrastructure projects worldwide.
Previous Post
Next Post
Related Articles
You Might Also Like
Quality Control Requirements for Ultra-Large Laser-Leveled Wear-Resistant Concrete Floors
Ultra-large laser-leveled, wear-resistant concrete floors combine precise laser leveling technology with the enhanced properties of wear-resistant materials. They are widely used in industrial plants, logistics warehouses, large commercial spaces, and other applications. Quality control must be implemented throughout the entire process: design, materials, construction, maintenance, and acceptance. The core goal is to achieve high flatness, high wear resistance, low cracking, and strong durability. The following details the quality control requirements from seven key perspectives: Ultra-large flooring (typically >1000 m2) is prone to cracking due to concrete shrinkage. Therefore, the initial design plan must focus on deformation control and construction feasibility. Specific requirements are as follows: Compartment Area: The size of a single compartment should be considered based on concrete shrinkage characteristics, typically ranging from 6m x 6m to 12m x 12m (aspect ratio ≤ 1.5) to avoid thermal stress cracking caused by excessive area. Joint Type Requirements: Expansion joints should be 8-12mm wide and ≥ 1/3 the floor thickness (or continuous). Use foam strips and sealant to prevent debris from entering and mitigate deformation. False Joint Installation: For long floors (e.g., >30m in length), false joints (cut depth 5-8mm) with intervals of ≤ 6m between compartment joints should be added to guide shrinkage cracks along the false joints. Clearly define the floor design elevation (±0.000 relative to the reference point). The laser leveling's reference line must be calibrated with a high-precision level (±1mm accuracy) to avoid cumulative errors. Flatness requirements: According to the "Code for Design of Building Floors" GB 50037, the allowable flatness deviation for industrial floors is ≤3mm/2m (laser detection), and for commercial floors, ≤2mm/2m. Strength Grade: Determined based on the application scenario. Industrial plants (load-bearing capacity 5-10t): ≥C30; logistics warehouses (load-bearing capacity >10t): ≥C35. Slump: Laser leveling requires low-slump concrete, controlled within 120±20mm (on-site measurement) to avoid delamination and sanding caused by excessive slump. Crack Resistance: Add polypropylene fiber (0.9-1.2kg/m³) or steel fiber (20-30kg/m³) to reduce plastic shrinkage cracking. Use a slow-setting water-reducing admixture to extend the initial setting time (≥6h) to ensure continuous construction over large areas. Material Type Core Control Indicators Inspection Requirements Commodity Concrete 1. Strength Grade (C30/C35); 2. Slump (120 ± 20 mm); 3. Initial Setting Time (≥ 6 hours); 4. Air Content (≤ 3%) One set of compression test blocks must be collected for every 500m³ of material. Slump must be measured on each truck upon arrival; any exceeding the standard must be immediately returned. Metal Wear-Resistant Materials 1. Metal Aggregate Content (≥ 60%, e.g., corundum, chromite sand); 2. Mohs Hardness (≥ 6); 3. Compressive Strength (≥ 80 MPa) Three sets of samples must be collected from each batch to test for hardness and strength. The appearance must be free of lumps and impurities. Non-Metal Wear-Resistant Materials 1. Quartz Sand Particle Size (0.3-1.2 mm, Continuous Grading); 2. Abrasion Resistance (Abrasion Loss ≤ 0.3 g/cm²); 3. Color Consistency Material within the same batch must exhibit no color variation. Abrasion resistance must be tested in accordance with GB/T 12988, "Test Method for Abrasion Resistance of Building Floor Materials." Auxiliary Materials 1. Polypropylene Fiber (Length 6-12 mm, Tensile Strength ≥ 300 MPa); 2. Sealant (Elastic Modulus ≥ 0.8 MPa) Fibers must be evenly dispersed and free of agglomerates. Sealant must comply with GB/T 14683, "Building Sealing Materials." Laser leveling is key to ensuring floor flatness. The entire "concrete paving – laser leveling – vibration – slurry preparation" process requires strict control. Specific requirements include: Construction Preparation and Equipment Calibration The concern laser leveling machine must be preheated one hour in advance. Use two independent reference points to calibrate the laser transmitter (with an error of ≤0.5mm) to avoid deviation from a single reference point. Base Preparation: The base layer (such as lime soil or gravel cushion) must be compacted (compaction degree ≥95%), with a surface flatness of ≤5mm/2m and no water accumulation or loose debris. Apply plastic sheeting (thickness ≥0.12mm) to prevent water absorption from the base layer, which could lead to rapid dehydration of the concrete. Paving Order: Divide the area by the gaps between the paving bays, and proceed from far to near, high to low, to avoid trampling on the already paved concrete. Thickness Control: Pave according to the designed thickness (usually 100-150mm) + 5% of the void thickness. Control the laser leveling speed between 0.8-1.2m/min, ensuring sufficient vibration with the vibrator (vibration frequency ≥ 50Hz) to remove air bubbles. Smoothness Monitoring: After every 50㎡ of paving, check the smoothness with a 2m straightedge and a feeler gauge. If the deviation exceeds 3mm, immediately use the laser leveling to level the surface. Manual repairs are strictly prohibited. Spreading and finishing of wear-resistant materials Spreading Timing: Before the concrete begins to set (press the concrete surface with your finger, leaving a 3-5mm indentation). Spread the concrete in two passes (60% for the first pass and 40% for the second pass) to avoid sinking if spread too early or preventing the concrete from bonding if spread too late. Spreading Uniformity: Use a "plum blossom dot" method with manual leveling to ensure the material dosage per square meter meets the design (usually 5-8kg/square meter for wear-resistant metals and 3-5kg/square meter for non-metals). Mechanical Finishing: After the first pass, smooth the surface with a disc trowel (150-200 rpm). After the second pass, finish the surface with a blade trowel (250-300 rpm). The surface should be free of smear marks, exposed areas, and have a uniform gloss. Large-scale floors are most susceptible to "plastic shrinkage cracks" (during construction) and "thermal shrinkage cracks" (during curing). These cracks must be controlled from three perspectives: Controlling Plastic Cracks During Construction Environmental Control: In high temperatures (>30°C) or strong winds (>5m/s), erect a sunshade and apply moisturizing spray (the temperature difference between the water and concrete should be ≤10°C) to prevent rapid surface water loss. Pre-setting Treatment: Within 30 minutes after paving, vibrate the concrete a second time using a vibrating beam to eliminate surface bubbles. If fine cracks are found, immediately re-press and close them with a trowel. Curing Time: 1-2 hours after finishing (initial setting of the surface), immediately cover with a moisture-retaining film and geotextile (or flame-retardant straw mat). Avoid direct sunlight exposure. Curning Time: ≥7 days for ordinary concrete, ≥14 days for concrete with admixtures or waterproofing. Water 3-4 times daily (keep the geotextile moist), and avoid sudden temperature drops. (If the temperature difference between day and night exceeds 15°C, cover with an insulation layer.) Post-Crack Treatment Fine cracks (width < 0.3mm): Seal with epoxy putty. Wide cracks (width ≥ 0.3mm): Cut a V-shaped groove (depth ≥ 10mm, width ≥ 8mm) along the crack, clean it, fill it with elastic sealant, and smooth the surface with wear-resistant material. After construction (during the curing period), the floor is susceptible to external damage and requires strict protective measures: Premature loading is prohibited: No personnel (except maintenance personnel) are allowed to move about within 7 days of curing, and no vehicles (including carts) are allowed to pass through within 14 days. Loading can only be carried after the floor has fully reached its design strength (28 days). Machinery protection: Machinery that requires operation on the floor (such as forklifts) must have rubber mats on their tires. Sharp turns and sudden braking are strictly prohibited to avoid scratching the surface. Pollution protection: Paint, engine oil, and other chemicals must not be piled on the floor. If spilled, rinse immediately with clean water (use a dedicated degreaser to remove oil stains) to prevent penetration and corrosion. Acceptance must be conducted in accordance with the "Concrete Structure Construction Quality Acceptance Code" (GB 50204) and the "Building Floor Construction Quality Acceptance Code" (GB 50209). Core testing items are as follows: Acceptance Items Quality Requirements Testing Methods: Smoothness Tolerance: ≤3mm/2m (industrial flooring), ≤2mm/2m (commercial flooring) Laser flatness tester (measure one point per 100 m2) or 2m straightedge + feeler gauge (measure three points per 50 m2). Abrasion Resistance Abrasion loss: ≤0.15g/cm² for metal wear-resistant flooring, ≤0.3g/cm² for non-metallic flooring Testing with an abrasion resistance testing machine in accordance with GB/T 12988 (measure one point per 1000 m2). Strength Concrete compressive strength: ≥ design value (C30/C35), surface hardness (rebound value): ≥35MPa (metal wear-resistant flooring) 28-day compression test of concrete specimens; surface hardness test with a rebound hammer (measure 10 points per 500 m2). Appearance Quality 1. No exposed surfaces, sanding, or hollows; 2. Uniform color variation (no significant differences within the same batch); 3. Crack width: <0.3mm Visual inspection (full inspection); tapping with a small hammer to detect hollows (measure 10 points per 100 m2, hollow rate ≤ 2%). Partition Joints/Expansion Joints Joint width and depth must meet design requirements, sealant must be fully applied without flaking, and no foreign matter must be present. Measurement with a tape measure (measure one point every 10 m); visual inspection of the sealant appearance. Common Problems Causes: Preventative Measures Surface Sanding 1. Excessive concrete slump; 2. Premature application of wear-resistant material; 3. Inadequate curing; Control slump at 120 ± 20 mm; apply wear-resistant material at the time of initial setting; apply moisturizing coating within 1 hour of finishing. Excessive Flatness 1. Uncalibrated laser leveling; 2. Uneven base layer; 3. Uneven paving thickness; Calibrate laser equipment (double reference points) before construction; compact and level the base layer (≤ 5 mm/2 m); apply paving according to the required thickness. Cracks (Width > 0.3mm) 1. Excessively large slab area; 2. Large temperature differences during curing; 3. High concrete shrinkage; Block size ≤ 12 m × 12 m; apply insulation when the temperature difference between day and night exceeds 15°C; incorporate polypropylene fiber to reduce shrinkage. Hollowing 1. Inadequate base layer cleaning; 2. Poor adhesion between concrete and base layer. Remove loose debris from the base layer and moisten it with water. When laying plastic film for insulation, partially cut the film to facilitate bonding. In summary, the quality control of ultra-large area laser-leveled wear-resistant concrete floors should focus on "prevention first, process control". Through strict material inspection, precise laser construction, and scientific maintenance and protection, the ultimate goal of "flatness, wear resistance, crack resistance, and durability" of the floor can be achieved. Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.Key points for purchasing second-hand power trowel and common methods to avoid pitfalls
Selecting a second-hand polishing machine is a job that requires a lot of experience and skills. It can help you obtain a practical device at a lower cost, but if you make a wrong judgment, the subsequent maintenance and delayed construction period may cause you to lose more than you gain. The following is a detailed list of key points for choosing a second-hand polishing machine and common methods to avoid pitfalls. We hope it can be of great help to you. Fuselage structure Chassis (grinding disc) : This is the most crucial part. Check if it is flat and free of deformation. Slight wear and tear is normal, but if the wear is severe, there are pits or obvious deformation, it will lead to poor polishing effect and higher replacement cost. Blade (scraper) : Check if there is still sufficient thickness. If the metal substrate has been worn out, it needs to be replaced immediately, and this cost should be included in the cost. Protective cover: Check for any damage or severe deformation, as this is related to operational safety. Overall framework: Check for any signs of welding, cracks or repairs, which could be a sign of severe impact or drop. Engine (heart) Brand: Give priority to well-known brands such as Honda, Kohler, Briggs & Stratton, etc. Spare parts are easy to find and maintenance is convenient. Appearance: Check for any cracks in the engine casing, especially in the base and radiator sections. Check for obvious oil stains or carbon deposits. This might be a sign of oil leakage or poor maintenance. Air filter: You can ask to remove the air filter to have a look. If the inside is very dirty or even soaked with oil, it indicates that the previous owner might not have paid much attention to maintenance. Engine oil: You can pull out the oil dipstick to check. If the engine oil is black, viscous or contains metal debris, it indicates that the engine wear may be relatively severe and the maintenance condition is poor. Transmission system Gearbox: Check if there are any signs of oil leakage on the gearbox housing. Rotate the drive shaft by hand to feel if it is smooth, and if there is any jamming or abnormal noise. Belt/chain: Open the protective cover and check if the belt has cracks, wear or looseness. Check if the chain is loose and free of oil and rust. Be sure to ask the seller to start the machine for testing! Startup performance Cold start is the most illustrative. Observe whether the rope pulling is smooth and whether the machine can start smoothly within one to three rope pulls. If it is difficult to start, there may be problems (such as carburetors, spark plugs, insufficient compression, etc.). Engine sound After starting, listen to the sounds of the engine idling and accelerating. The operation should be smooth. A regular "tap-tap" sound is normal (valve sound). If there are loud "clicking" sounds, knocking sounds or irregular noises, it indicates that there is severe wear inside. Transmission system sound Let the trowel run idle and listen for any abnormal "clattering" sounds from the gearbox and transmission parts. The voice should be even and deep. Vibration condition When the machine is running, it should be smooth and the vibration should be within a reasonable range. If the vibration is abnormally severe, it may be due to deformation of the chassis, unbalanced installation of the blades or problems with the engine base Purchase time and source: Inquire about the specific year and channel of purchase of the machine to determine its service life. Usage frequency and scenarios: Is it for occasional household use or long-term high-intensity use by professional teams? The latter naturally wears out more severely. Maintenance and repair history: This is of Paramount importance. Has there been any major overhaul? (Such as engine cylinder opening, gearbox replacement When was the last time the engine oil, air filter and spark plugs were changed? Have there been any accidents (such as tipping over or collision)? A reliable seller will tell the truth, while a evasive one needs to be on guard. If possible, conduct a brief load test (such as grinding it on the ground). Observe after the load is applied: Whether the engine is prone to stall and whether the power is sufficient. Check for any slippage or abnormal noise in the transmission system. Whether the machine moves smoothly and if it deviates. Trap description: Merchants thoroughly clean and paint the machines to make their appearance look as good as new, thereby covering up internal wear and tear and malfunctions. Avoidance methods Pay special attention to the screws and interfaces: It is very difficult for a refurbished machine to have no signs of any screws being turned. Check whether there are any signs of wear on the engine fixing screws, chassis screws, etc. Paint surface consistency: The original factory paint surface is usually uniform. If you find that the paint color of some parts does not match the overall color or the paint layer is too thick, it might be due to later spraying. Don't judge a machine by its appearance: Don't be deceived by a clean exterior. The key is to check its operating status and internal wear. Trap description: The machine was once sold after its chassis and frame were deformed due to a fall or collision. It was sold after simple repairs. Avoidance methods Check the flatness: Place the machine on a flat ground and observe from the side whether the chassis is fully in contact with the ground and if there is any warping. Check the welding points: Carefully inspect each connection point of the rack to see if there are any irregular or rough welding points in the later stage. Running test: During no-load operation, observe whether the machine is stable and if there is any regular swinging. This might be a sign of an uneven chassis. Trap description: Piecing together a complete machine with "good" parts from different scrapped machines, which has poor compatibility and stability. Avoidance methods Brand consistency: Check whether the brand, model and newness of the main components such as the engine and fuselage match. Assembly machines often give the impression of being "mismatched". Check the nameplate: Whether the information on the body nameplate (such as model and production date) is consistent with the seller's description. Poor comprehensive operation: When the assembly machine is in operation, various minor problems may occur frequently, making it feel "not smooth". Trap description: The machine performs okay when it is cold or unloaded, but once it is heated up or loaded, problems become apparent (such as insufficient power, severe abnormal noises, and engine stalling). Avoidance methods Persist in long-term testing: Let the machine run for 10 to 15 minutes and observe whether the state is stable after warming up. Load testing is required: This is the best way to verify the true state of the machine. Check the engine oil: After warming up the machine, stop it immediately and check the engine oil. If there are many small bubbles (emulsions) in the engine oil, it might be that the cylinder gasket is being washed away, which is a big problem. Before deciding to purchase, quickly check the following list: Inspection items Qualification standard Be cautious/give up Fuselage chassis Smooth, evenly worn, and without deformation Deformation, cracks, wear limit Engine Well-known brand, smooth start-up, stable operation, pure sound, no oil leakage Difficult to start, severe abnormal noise, oil leakage, and heavy smoke Transmission system The rotation is smooth without any abnormal noise, and the belt/chain is not aged There is abnormal noise, jamming and oil leakage Seller Description Be honest, answer all questions, and keep clear maintenance records Vague and evasive, concealing history Price In line with market conditions (approximately 30% to 50% of a new model) Far below the market price (" There's no such thing as a free lunch ") Test run situation The hot and cold units start well and operate stably under no-load or load conditions Any test is unqualified Final suggestion: If possible, bring along an experienced master craftsman or mechanic. Their experience can help you discover many problems that beginners fail to notice. When making a purchase, it is best to sign a simple written agreement with the seller, clearly stating the condition of the machine, and keep the payment voucher for unexpected needs. Remember, the primary principle when purchasing second-hand equipment is "It's better to miss out than to buy wrongly." Wish you could find a sturdy and durable good machine! Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.From Ground Up: Your Complete Guide to Professional Concrete Slab Preparation & Pouring
Whether you're planning a sturdy new patio, a warehouse floor, or any concrete project, success is truly built from the ground up. A flawless finish begins long before the concrete truck arrives. At Vanse Machinery, with over a decade of expertise in concrete equipment, we understand that proper ground preparation is the most critical, yet often overlooked, step. This comprehensive guide will walk you through the essential stages of prepping for a concrete slab and introduce how modern robotic concrete pumps and laser-guided equipment can elevate your project's quality and efficiency. A concrete slab is only as strong and stable as the base it rests on. Skipping or rushing through preparation is a direct path to future cracks, sinking, and expensive repairs. Here is your essential checklist for how to prep ground for concrete slab: Site Clearing & Excavation: Remove all vegetation, topsoil, rocks, and debris. Excavate to the required depth, accounting for the slab thickness and the sub-base material. Sub-Grade Compaction: Compact the native soil thoroughly. A well-compacted sub-grade prevents settling. For optimal support, consider using a laser leveling machine to ensure a perfectly flat and uniform base before adding gravel. Installing the Sub-Base: Add a 4-6 inch layer of compactible gravel or crushed stone. This layer provides drainage, prevents frost heave, and offers a stable platform. Use a plate compactor in layers to achieve maximum density. Formwork & Reinforcement: Build sturdy wooden or metal forms to define the slab's edges. Install any necessary reinforcement, such as rebar or welded wire mesh, and support it with chairs to keep it centered in the slab. Final Checks & Moisture Barrier: Verify all dimensions, levels, and slopes. On indoor projects or where moisture is a concern, lay a vapor barrier over the sub-base before pouring. While meticulous manual preparation is vital, the actual pouring and finishing phases are where modern concrete pouring equipment makes a transformative difference. This is the core of Vanse's expertise. For Unmatched Flatness: Laser Leveling Technology After the concrete is placed, achieving a perfectly level surface is paramount. Vanse's Boom Laser Leveling Machines (like the YZ30-4E) automate this process. They use a rotating laser transmitter and a mobile receiver to automatically control the Leveling head's height, producing a super-flat floor with far greater speed and accuracy than manual methods. This technology is essential for large-scale industrial floors, warehouses, and commercial spaces. Beyond Basic Pumps: The Power of Robotic Placement The keyword robotic concrete pump points to the future of placement. Vanse's advanced machinery embodies this concept. Our truck-mounted concrete boom pumps allow for precise, remote-controlled placement of concrete directly into the forms, even in hard-to-reach areas. This minimizes labor, reduces material segregation, and significantly speeds up the concrete pouring process for patios, foundations, and elevated slabs. From Pour to Polish: The Complete Equipment Ecosystem A perfect slab requires more than just pouring. Vanse provides the full suite of equipment: Spreaders & Distributors: For evenly placing and roughly leveling the concrete mass. Power Trowels: Ride-on and walk-behind models (like the VS836) for creating a dense, smooth, professional-grade finish. Cutting Machines: To create precise control joints (like those made with the VS-HM500), which guide where the concrete should crack as it cures, preventing unsightly random cracks When you research cement slab preparation, you're seeking reliable, proven solutions. This aligns perfectly with Google's E-E-A-T (Experience, Expertise, Authoritativeness, Trustworthiness) framework, which Vanse exemplifies: Experience & Expertise: Founded in 2013, Vanse is a national high-tech enterprise with deep, specialized knowledge in concrete equipment R&D and manufacturing. Our solutions are born from real-world application. Authoritativeness: We have successfully partnered with major global firms like JD Logistics, CATL, and China State Construction Engineering Corporation (CSCEC), a testament to the reliability and performance of our equipment on demanding projects. Trustworthiness: Our global reach-exporting to over 80 countries including the USA, Germany, Australia, and Saudi Arabia-and established overseas branches demonstrate a commitment to quality and international standards that contractors worldwide trust. Preparing for a concrete slab is a systematic process that blends fundamental best practices with cutting-edge technology. By following a thorough concrete pre pour checklist for ground preparation and leveraging precision equipment like laser Levelings and advanced pumps for the pour, you ensure a result that is structurally sound, aesthetically pleasing, and built to last. For contractors and project managers looking to invest in efficiency and quality, exploring Vanse's range of concrete pouring equipment is the logical next step. Our team is ready to help you select the right machinery to make your next patio, floor, or slab project your most successful one yet. Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.