Technical Knowledge
Know about the 20/30/40 rule in concrete
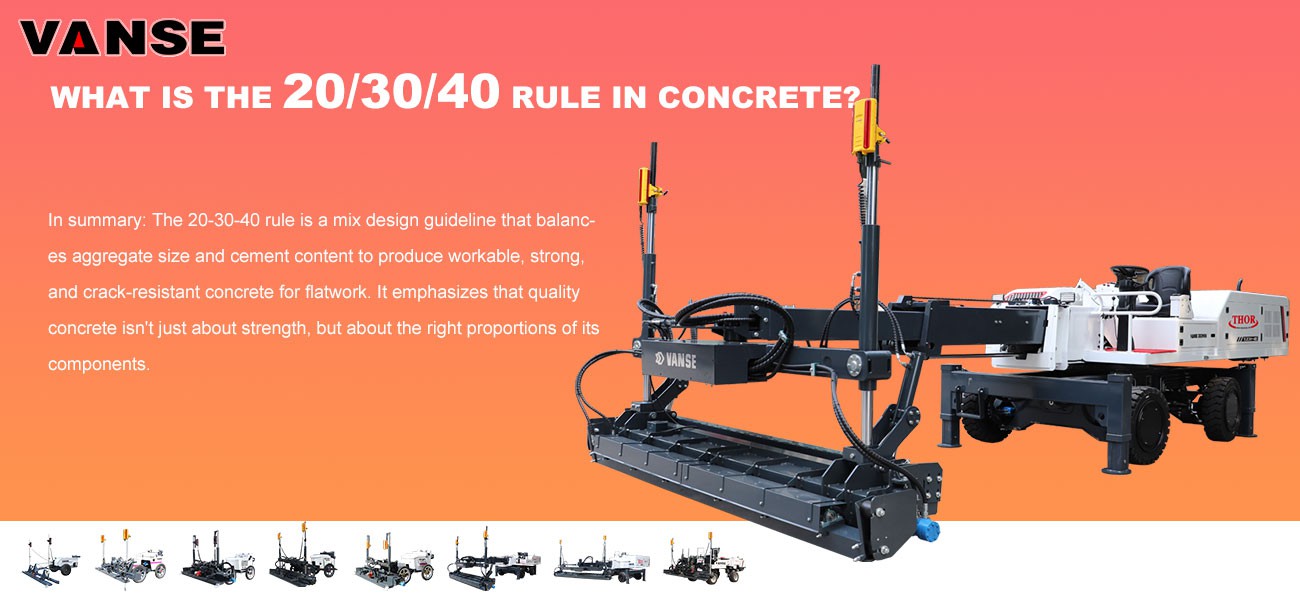
The 20-30-40 rule in concrete is a crucial guideline, primarily used for flatwork projects like driveways, sidewalks, patios, and slabs. It refers to the general specifications for the aggregate (stone) size within the concrete mix.
Here’s what each number means:
| Number | Meaning | Typical Application |
| 20 | The maximum aggregate size should be 20 mm (about 3/4 inch). | This ensures the mix can flow properly around rebar and into forms without creating voids or honeycombing. It's a standard size for general-purpose concrete. |
| 30 | The average aggregate size is around 30 mm (about 1 1/4 inch). | This indicates the mix uses a gradation of stones, with an average size larger than the maximum to ensure good interlock and strength. |
| 40 | The minimum cement content should be 40 kg per cubic meter of concrete. | This guarantees sufficient cement paste to coat all aggregates, bind them together, and achieve the desired strength and durability. |
The "Rule" in Plain Language:
Essentially, it's a shorthand for specifying a strong, workable, and durable concrete mix by controlling:
How big the biggest rocks can be (20mm max).
The general size of the mix of rocks (30mm avg).
How much "glue" (cement) is in the mix (40kg minimum per m³).
Important Caveats and Context:
It's a Guideline, Not an Absolute Law: Exact mix designs are determined by structural engineers based on compressive strength (e.g., 3000 psi, 4000 psi), exposure conditions (freeze-thaw, sulfates), and placement method. The 20-30-40 rule provides a good starting point for typical residential and light commercial flatwork.
Local Standards Vary: In the US, specifications are often in psi strength and slump rather than this exact ratio. However, the principle is the same: control aggregate size and cement content for performance.
Common Related "Rules": You may also hear the "20-20 Rule" for placing concrete, which states:
Slump should be a maximum of 20 cm (8 inches). (Too wet leads to shrinkage and cracking).
The maximum aggregate size should be 20 mm (3/4 inch).
Purpose: This rule helps prevent common problems:
Too large aggregate: Makes finishing difficult and can cause surface flaws.
Too little cement: Results in weak, permeable, and non-durable concrete.
Practical Takeaway for Homeowners & DIYers:
When ordering concrete for a project like a driveway, you can use this rule as a checklist when talking to your ready-mix supplier. You might say:
*"I need a 4000 psi mix for a driveway, with a 3/4" max aggregate and a 4-5 inch slump."*
This communicates the same intent as the 20-30-40 rule-you're asking for a mix with appropriately sized stone and sufficient cement for a strong, durable finish.
IN SUMMARY: The 20-30-40 rule is a mix design guideline that balances aggregate size and cement content to produce workable, strong, and crack-resistant concrete for flatwork. It emphasizes that quality concrete isn't just about strength, but about the right proportions of its components.
Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.
Thanks to All the Friends Who Support and Trust Shandong Vanse Machinery Technology Co., Ltd.
If you want to know more about Shandong Vanse Machinery Technology Co., Ltd. or have any questions, please feel free to contact us:
Our Factory
Shandong Vanse Machinery Technology Co., Ltd.
Share this article
About the Author: Shandong Vanse Machinery Technology Co., Ltd.
Shandong Vanse Machinery Technology Co., Ltd. is a high-tech manufacturer specializing in concrete construction machinery, including laser screeds and related equipment. The company integrates R&D, production, and global sales, with products exported to over 60 countries and widely used in infrastructure projects worldwide.
Previous Post
Next Post
Related Articles
You Might Also Like
Large area concrete laser leveling diamond wear-resistant floor and corrugated compartment joint anti-cracking construction method
1. High-precision leveling: – With the help of a concrete laser leveling machine, the operation is carried out based on the precise plane reference formed by the laser beam. The laser receiver feedbacks the deviation information in real time, and the leveling machine automatically and accurately adjusts the scraper height and vibration frequency to ensure that the floor flatness error can be controlled within a very small range, usually within ±2mm, providing a solid foundation for subsequent processes, especially suitable for precision manufacturing workshops, high-end storage facilities and other places with strict requirements on flatness. 2. Excellent wear resistance: – In the initial setting stage of concrete, diamond wear-resistant materials are evenly spread. With its high hardness and high strength, it is closely integrated with the surface of concrete. After smoothing and finishing, a solid and wear-resistant protective layer is formed, which greatly improves the wear resistance of the floor, effectively copes with high-intensity wear scenes such as heavy-loaded vehicles and frequent cargo handling, and significantly extends the service life of the floor. 3. Unique corrugated compartment joint design: – Abandoning the traditional straight compartment joint, the corrugated compartment joint is adopted. This design not only meets the needs of concrete expansion and contraction and prevents cracks, but also has a better stress dispersion effect than the straight joint, which can effectively reduce the risk of cracks caused by uneven foundation settlement and temperature changes. It can also add a unique visual beauty to the floor and enhance the overall image of the site. 4. High efficiency of construction: – All construction links are closely connected, from base treatment, concrete pouring, laser leveling, to wear-resistant material spreading, compartment joint setting and subsequent maintenance, all in one go and in an orderly manner. Laser leveling technology greatly improves the leveling efficiency. Compared with traditional manual leveling methods, the construction speed can be increased several times, which greatly shortens the overall construction period and reduces the project construction cost. It is widely used in various large-scale and high-load indoor and outdoor concrete floor projects, such as large industrial plants, logistics distribution centers, airport aprons, exhibition halls, port terminal cargo yards and other places, especially for projects with high requirements for floor flatness, wear resistance and crack resistance, and the expectation of a certain aesthetics. 1. Laser leveling principle: – The laser transmitter releases a rotating laser beam to form a high-precision horizontal control surface. The laser receiver installed on the leveling machine continuously captures the laser signal, compares the real-time elevation of the floor with the laser reference surface, and transmits the generated deviation signal to the control system, prompting the hydraulic mechanism of the leveling machine to respond quickly, accurately control the scraper, vibrator and other components, and realize fast and accurate leveling and vibration of the concrete, achieving a high-precision leveling effect. 2. The wear-resistant principle of corundum: – When the concrete is in the initial setting state and the surface has a certain viscosity, the spread corundum particles can be embedded in the surface of the concrete. With the subsequent leveling and finishing operations, the corundum is deeply combined with the concrete. With its excellent hardness and wear resistance, it builds a solid defense line against wear on the concrete surface, protecting the main structure of the floor from friction loss in daily use. 3. The anti-cracking principle of the corrugated compartment joint: – Compared with the straight joint, the curved shape of the corrugated compartment joint can more effectively disperse the stress during the expansion and contraction of the concrete. When the concrete needs to expand and contract due to factors such as temperature rise and fall and foundation settlement, the corrugated joint guides the stress to disperse along the curve to avoid excessive stress concentration, thereby reducing the possibility of cracks and ensuring the integrity and stability of the floor. 1. Construction preparation: – Technical preparation: Read the construction drawings in detail, clarify the technical requirements, prepare a rigorous construction plan, and organize construction personnel to conduct technical briefings. – Site preparation: Thoroughly clean up debris and accumulated water on the construction site, ensure that the base is flat, and take reinforcement measures for weak bases; reasonably plan the temporary drainage system for construction; design the concrete pouring and leveling route and the layout of the compartment joints according to the shape and area of the site. – Material preparation: Strictly purchase high-quality cement, sand, admixtures, diamond wear-resistant materials, etc. according to design requirements, strictly inspect the raw materials to ensure that the quality meets the standards; prepare sufficient water and electricity for construction. – Equipment preparation: Comprehensively debug concrete laser leveling machines, concrete mixing equipment, transportation equipment, wear-resistant material spreaders, trowels, etc. to ensure that the equipment is in good operating condition; accurately calibrate the laser system to ensure that the emitted laser plane matches the floor design elevation. 2. Base treatment: – Deeply clean the base to remove dust, oil and other pollutants; compact the base with a roller or compacting machine, with a compaction degree of not less than 90%; use concrete or mortar to repair and level the local potholes and holes on the base, so that the base leveling error is controlled within ±10mm. 3. Concrete pouring: – Accurately weigh the raw materials according to the designed mix ratio, use a forced mixer to fully mix the concrete, and the mixing time is not less than 90 seconds to ensure the uniformity of the concrete; use pumping or self-unloading to transport the concrete to the construction area, control the pouring speed, prevent concrete segregation, and the pouring thickness should be slightly higher than the designed floor elevation by 10-20mm to reserve operating space for subsequent leveling. 4. Laser leveling: – Turn on the laser leveling machine and keep moving at a constant speed, usually controlled at 1-2m/min; the operator flexibly adjusts the scraper height and vibration frequency of the leveling machine in real time according to the signal fed back by the laser receiver to ensure that the concrete surface is flat and vibrated densely; the leveling work of adjacent areas must be completed before the initial setting of the concrete, and the overlapping construction width must be no less than 10cm to ensure the integrity of the floor. 5. Spreading of wear-resistant materials: – When the concrete is initially set (generally there are slight footprints when stepping on it, and the sinking depth is about 3-5mm), use a special spreader to evenly spread the diamond wear-resistant material on the floor surface according to the specified amount, and the spreading thickness is approximately 3-5mm; during the spreading process, the spreading speed and direction must be accurately controlled to prevent the accumulation or leakage of wear-resistant materials, and ensure that the spreading uniformity reaches more than 90%. 6. Smoothing and finishing: – After the wear-resistant material is spread, use the trowel to smooth it immediately. The trowel should be operated in a crisscross pattern to make the wear-resistant material fully blend with the concrete. The number of smoothing times should be no less than 3 times. As the concrete continues to harden, when there is no water stain on the surface and it feels slightly hard when pressed with fingers, it should be smoothed manually. Aluminum alloy rulers, trowels and other tools should be used to make the floor surface bright and smooth. 7. Corrugated compartment joint setting: – Before the concrete is finally set, according to the pre-designed compartment joint layout, a special mold or cutting equipment is used to make a corrugated compartment joint. The mold or cutting tool should ensure that the depth of the joint reaches 1/3 – 1/4 of the thickness of the concrete slab, and the joint width is controlled at 5 – 10mm. During the production process, the shape of the joint should be regular and smooth, and the anti-cracking and aesthetic functions of the compartment joint should be effectively exerted. 8. Maintenance: – After finishing and setting the compartment joints, the floor shall be maintained in time by covering with plastic film, spraying curing agent or laying water straw mats, etc. The maintenance time shall not be less than 7 days. During this period, the concrete surface must be kept moist to avoid cracks caused by water loss; warning signs shall be set up during the maintenance period, and vehicles and pedestrians are strictly prohibited from passing on the floor that does not meet the strength requirements. 1. Flatness Quality Control: – Before construction, use professional instruments to finely calibrate the laser system to ensure the accuracy of the laser plane; during the construction process, regularly use a 2m ruler and feeler gauge to check the flatness, at least once every 100-200 square meters, and adjust the leveler immediately if deviation is found; after finishing, use a laser flatness meter to comprehensively test the flatness of the floor to ensure that it meets the design requirements. 2. Wear-resistant performance quality control: – Select diamond abrasive wear-resistant materials strictly according to design requirements, and carefully check quality certification documents; in the spreading process, strengthen on-site supervision to ensure that the spreading amount and uniformity meet the standards; after maintenance, on-site wear resistance tests can be carried out, such as grinding a certain area with a grinding wheel, observing the wear condition, and judging whether the wear resistance meets the standards. 3. Partition seam quality control: – When making partition seams, strictly control the depth, width and shape of the seams, and use precise measuring tools for inspection; regularly inspect the partition seams to check whether there are debris blocking them. If problems are found, clean and repair them in time to ensure that the partition seams function normally. 1. Organize construction personnel to participate in safety training to familiarize them with the operating specifications and safety precautions of various construction equipment (such as laser leveling machines, concrete mixers, cutting equipment, etc.). 2. Set up safety warning signs in conspicuous locations on the construction site to clearly divide the construction area and non-construction area to prevent unrelated personnel from entering the construction danger zone. 3. Regularly conduct safety inspections on construction equipment, focusing on electrical insulation, mechanical protection devices, etc., to ensure the safe operation of equipment and prevent safety accidents caused by equipment failure. 4. Provide construction personnel with complete personal protective equipment, including safety helmets, safety shoes, gloves, etc., to ensure the personal safety of construction personnel. 1. Classify and collect solid waste such as concrete residues and discarded diamond abrasive material packaging bags generated during the construction process, and regularly transport them to designated garbage disposal sites. 2. Reasonably plan construction time, avoid high-noise concrete mixing, equipment operation and other operations during residents' rest periods, and take noise reduction measures when necessary, such as installing silencers on equipment. 3. Strengthen the control of dust on construction sites, cover material storage sites, close transport vehicles, regularly sprinkle water to reduce dust, and maintain a clean environment on the construction site. 1. Economic Benefit: – High-precision laser leveling combined with efficient construction process greatly shortens the construction period and reduces labor, equipment rental and other cost expenditures; diamond abrasive wear-resistant floor reduces the cost of later maintenance and floor replacement; corrugated compartment seams reduce the cost caused by crack repair, and the comprehensive economic benefits are significant. 2. Social Benefit: – Provide high-quality floor solutions for large-scale industrial, logistics and other projects to meet the needs of industry development; reduce construction noise, dust and other pollution, and help environmental protection and urban sustainable development. In a large automobile manufacturing plant construction project, this construction method was used, with a construction area of more than 80,000 square meters. The floor flatness error is precisely controlled within ±1.5mm, meeting the requirements for the installation of precision equipment on the automobile production line; the diamond abrasive wear-resistant layer effectively resists the wear caused by the transportation of production equipment and vehicle driving; the corrugated compartment seams are beautiful and have no cracks, providing a solid guarantee for the efficient and stable operation of the plant, and have been highly praised by the owner. For example, in the renovation project of a busy port terminal cargo yard, this construction method also achieved remarkable results. A large area of floor was quickly built with excellent wear and crack resistance, which met the high-intensity operation needs of the port and greatly improved the cargo yard operation efficiency.How does the concrete curing agent maintain the flatness of the laser-tilled floor during the curing process?
The concrete curing agent itself does not directly create a smooth surface. Its main function is to "protect" the precise smoothness already achieved by the laser leveling machine by controlling the loss of moisture, preventing it from deforming or being damaged during subsequent curing and hardening processes. The laser leveling machine lays a highly precise horizontal foundation for the ground. The curing agent is like an invisible "shield" that ensures this foundation is not damaged by factors such as contraction and warping. Its specific mechanism of action mainly manifests in the following two aspects: This is the most crucial approach for the protective flatness of the sealant. During the hardening process of concrete, if the moisture evaporates too quickly, it will generate huge internal stress, leading to two serious consequences that severely affect the flatness: Reducing shrinkage cracks: When the pore water inside the concrete evaporates to form a crescent surface, its surface tension will exert a pull on the pore walls, causing the concrete to shrink. If the shrinkage is not uniform, cracks will form, damaging the integrity of the floor. The sealant (especially the shrinkage-reducing type) can effectively reduce the surface tension of the pores, thereby reducing the drying shrinkage by 80% (28 days) to 50% (1 year or longer), eliminating the destructive force caused by shrinkage at its source. Preventing board warping: When the drying speeds of the upper and lower surfaces of the concrete slab are inconsistent (such as the upper surface drying faster and the bottom surface drying slower), warping occurs, that is, the edges or corners of the slab rise upwards. This is the number one killer of flatness. The moisture-retaining film formed by the sealant ensures that the slab surface is uniformly hydrated, minimizing this deformation caused by the humidity gradient. It has been reported that using the appropriate curing product can increase the spacing of the joint (the gap reserved to cope with shrinkage) and achieve a smoother and more durable floor. Some advanced curing agents, especially those that can be used during the finishing process, can also assist in achieving a smoother surface by optimizing the construction: Extended operation time: In hot or windy conditions, the concrete surface tends to harden too quickly, resulting in incomplete finishing and leaving knife marks or waves. Curing agents can slow down the evaporation of surface moisture, providing construction workers with a longer operation window, allowing them to make the floor smoother with more ease. Reduced finishing damage: High-quality curing agents can act as a lubricant, reducing the dragging force of the trowel on the concrete surface. This helps to reduce parallel micro-cracks beneath the surface and enables more precise seam cutting, preventing damage to the surface's smoothness due to improper finishing. This issue touches upon a crucial point. Based on your question, you may have come across various types of products, and they do have differences: Product type Main mechanism of action Contribution to flatness Traditional/membrane-forming curing agent Form a physical film on the surface of the concrete, locking in moisture. Passive protection: Through moisturization, it prevents shrinkage and cracking caused by excessive water loss, thereby maintaining the existing flatness. Reactive/permeation-type curing agent Penetrate into the concrete interior, react with the cement hydration products, fill the capillary pores, and play a role in densification and assisting in hydration. Active enhancement: In addition to moisturization, it can directly reduce micro-cracks and act as a finishing aid to improve construction quality, thus achieving a more excellent flatness effect. Retarding agent Added internally to the concrete, it reduces the surface tension of pore water at its source, significantly reducing shrinkage during drying. Root cause control: This is the most fundamental solution. By minimizing the contraction stress to the lowest level, it completely prevents flatness problems caused by contraction, allowing for a larger joint spacing. In summary, the concrete curing agent achieves the maximum reduction of volume changes and stress during the hardening process of concrete through both moisture-retaining curing and chemical shrinkage. This ensures that the high-precision results of laser leveling can be perfectly "locked" and preserved, ultimately resulting in a long-lasting, flat, and durable high-quality floor. Does your project have specific numerical requirements for the floor's flatness (such as FF/FL grades)? Also, is the floor planned to undergo sealing curing or polishing treatment? This will directly affect the selection of the curing agent. Some curing agents have better compatibility with subsequent coatings, while others are specifically designed for polishing systems. Please provide these details so that I can confirm if the current choice is the most suitable. Contact us NOW Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.What are some common troubleshooting steps for laser system failures?
The laser system of the concrete laser leveling is the core for achieving high-precision screing. Once a malfunction occurs, it will lead to a decrease in the leveling accuracy and affect the construction quality. The following are systematic and common troubleshooting steps. It is recommended to follow the principle of "from simple to complex and from outside to inside". Stop the machine immediately: Turn off the leveling machine and make sure the laser emitter is also turned off to prevent the laser from causing harm to the eyes. Confirm whether the battery power of the laser transmitter and receiver is sufficient. Low battery power can cause unstable signals. Check all cables and plugs for any damage, looseness or poor contact (especially the connection line between the receiver and the main unit of the leveler). Laser receiver: Clean its sensing panel to ensure there is no cement slurry, dust or oil stains covering it. Laser emitter: Clean the emission window to ensure the lens is clean. Mast/Benchmark: Check whether the mast on which the receiver is installed is vertical, stable and free from deformation. Confirm the status of the transmitter Make sure the laser emitter is turned on and in the rotating (sweeping) mode. Check if it is level (observe the bubble level it comes with). Listen to the sound and observe: During normal operation, there should be the sound of the motor rotating, and a moving red dot can be seen on the obstacle when the laser beam appears. Height and position inspection Height: Ensure that the receiver is within the effective working height of the laser plane (usually, the laser plane is best at the middle position of the receiver's sensing rod). If the receiver is too high or too low, no signal will be received. Location: Move the receiver directly near the laser emitter to see if there is a signal. If it is present near but not far away, it might be that the laser plane is blocked or the emitter is not level. Interference screening Check whether there is strong direct sunlight, other laser equipment or strong light source interference in the work area. Try to cover the receiver with a light shield. Equipment replacement test (if conditions permit) : Test with a confirmed normal receiver, or take the faulty receiver to another normally working transmitter for testing. This can quickly determine whether the fault point is the transmitter or the receiver. Inspect the ground and foundation Is the laser emitter tripod set up on a solid and stable ground? The vibration or subsidence of the ground during the pouring process can cause the launcher to shake. Check whether the leveling machine itself shakes violently when moving. Check the mechanical connections Is the connection between the receiver and the mast, as well as the connection between the mast and the body of the leveling machine, firm? Any loosening will cause signal jitter. Check whether the connection hydraulic cylinder/hinge point between the scraper or rammer plate of the leveling machine and the body is too loose, causing free travel. Electrical interference Lay the cables of the laser system separately from the main power line and hydraulic line of the leveling machine to avoid parallel and close contact, so as to reduce electromagnetic interference. Environmental review Is there a large amount of dust and steam in the air? These will scatter laser, causing the signal to weaken and become unstable. High-temperature heat waves can also cause light refraction. Calibration check (the most common cause) : Transmitter calibration: Use the dedicated calibration tool provided randomly and follow the steps in the manual to check and calibrate the horizontal accuracy of the laser transmitter itself. This is the most crucial step. Receiver zero point calibration: At a reference point of known height (such as a pre-set reference post), perform the operation of "zeroing" the receiver or setting the reference height. Reference point and setting check Recheck whether the construction reference point (elevation) is accurate and whether the height set on the transmitter is correct. Confirm whether the mode selected on the control panel of the leveling machine (such as the "Leveling" mode) is correct. Mechanical system linkage inspection After the laser system gives the correct signal, check whether the hydraulic lifting system of the leveling machine responds promptly and accurately. Are there any problems such as clogged hydraulic valves or leakage inside the cylinder? The lifting action can be manually operated to test whether it is smooth and powerful. If none of the above steps can solve the problem, it may involve an internal fault: Transmitter: Internal level sensor failure, motor drive module damage, laser tube aging, etc. Receiver: Damaged sensing element, mainboard failure, etc. Contact the equipment supplier or professional maintenance personnel. Provide detailed fault phenomena and the troubleshooting steps that have been taken. Do not disassemble the core components of the laser emitter or receiver by yourself, especially since the laser emitter has precise optical components and high-precision sensors inside. Non-professional disassembly may lead to permanent damage or calibration failure. Proper storage: After use, clean the equipment thoroughly and store it in a dry, shockproof toolbox. Regular calibration: In accordance with the requirements of the operation manual, conduct official calibration of the laser system on a regular basis (such as every quarter or before the start of each major project). Battery management: Use original or high-quality batteries. Remove the batteries when not in use for a long time. Avoid impact: Handle with care to prevent the laser equipment from being subjected to severe impacts or drops. Observe the fault phenomenon → Power off for safety inspection → Cleaning and appearance inspection → Power supply and wiring inspection → Select the above path for troubleshooting based on the phenomenon (no signal/unstable/poor precision) → Try to replace the component for testing → Contact professional maintenance. Through the above systematic steps, the vast majority of common faults of the laser system of the concrete laser leveling can be solved. Note: The parameters provided in this document are for reference only and are not mandatory. Due to differences in technical characteristics between different brands and models of laser levelers, please consult the manufacturer for a suitable solution before actual operation. This reference document assumes no responsibility for any issues arising from failure to follow the manufacturer's instructions.